

For the bright spots, bright marks, bright spots caused by improper application of double bonding oil on double bonded surfaces, we can divide them into several key problems and propose solutions for them respectively.
Problem segmentation and definition:
Problems of double-heating oil: double-heating oil film strength is insufficient or uneven roll surface, resulting in uneven distribution of oil film in the rolling process.
Rolling process problems: rolling process due to uneven oil film, resulting in uneven rolling deformation, resulting in bright spots, bright marks, bright spots.
Incoming material and roll problems: incoming material cleaning is not clean or roll roll surface is not uniform, further aggravate the rolling process problems.
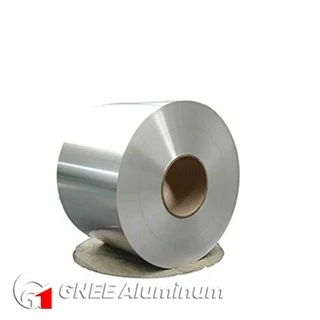
| Product Name | Aluminum Foil Roll |
| Item | Supplier Catering Aluminium Foil, Silver Aluminium Foil Paper, Food Packing Household Aluminium Foil |
Type |
Heavy gauge foil, Medium gauge foil, Light gauge foil |
Alloy Type |
1050, 1060, 1070, 1100, 1235, 3003, 3004, 5052, 8006, 8011, 8021, 8079 |
Thickness &Tolerance |
0.006 ~ 0.2mm |
Width |
10mm ~ 1500mm |
Temper |
O ~ H112 |
| Application | Medicine packaging, food packaging, Aluminum foil tape, Meal box materials, Drug capsules, Tape foil, etc |
MOQ |
3 ton |
Sample |
Free |
Delivery Time |
7-25 days after order confirmation |
Loading Port |
Qingdao Port,Tianjin Port,Shanghai port, etc. |
Price Terms |
FOB, CIF, CFR, CNF, etc. |
Standard |
ASTMB209,EN573-1S, etc |
Certificate |
ISO, RoHS, etc |
Our Service |
We can provide you with free samples and various custom services. |
Solution:
1. Double-compound oil problem solution:
Selection of suitable double oil: select the double oil with high film strength and good stability to ensure even distribution of oil film in the rolling process.
Regularly check the double oil: regularly check the quality of the double oil to ensure the stability of its performance, and timely replacement of unqualified oil.
2. Rolling process problem solving method:
Optimise the rolling parameters: adjust the parameters such as the amount of underpressure and rolling speed to ensure even distribution of rolling force in the rolling process and avoid uneven rolling.
Regular inspection of rolls: Regular inspection and maintenance of rolls to ensure that its surface is flat, no damage to ensure the stability of the rolling process.
3. Incoming material and roll problem solution:
Strengthen the incoming material cleaning: to ensure that the incoming material in the rolling before a thorough cleaning to remove the surface oil, impurities, etc., in order to reduce the rolling process of foreign matter pressed into.
Optimise roll treatment: regular grinding and polishing of the rolls to ensure that their roll surface is uniform and smooth, to improve the stability of the rolling process.
Summary:
Through the selection of suitable double-compound oil, optimization of rolling parameters, strengthening incoming material cleaning and optimization of roll treatment and other methods, can effectively solve the double-compound surface due to improper application of double-compound oil caused by the bright spots, bright marks, bright spots. At the same time, these methods also help to improve the stability of the rolling process and product quality.
*** Translated with www.DeepL.com/Translator (free version) ***